-
ABOUTThe group company integrates design, casting, production, research and development, sales and service to provide customers with modern, digital one-stop water supply system solutions.

-
PRODUCTS
-
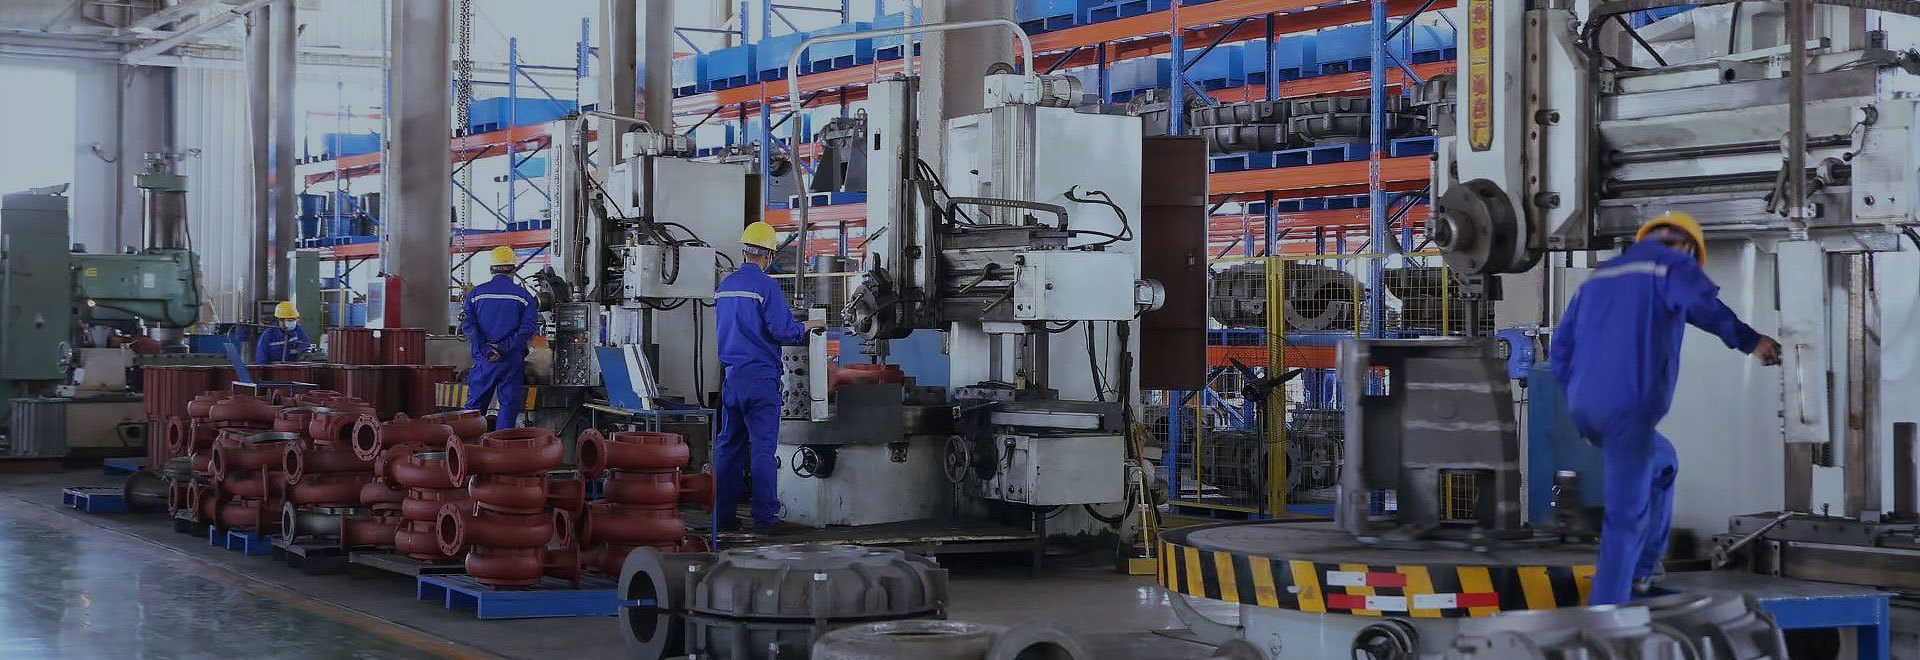
APPLICATION4 production bases in group company, 10 branches, more than 20 offices, more than 1000 professional employees, long-term service to domestic and foreign high-end customer groups including Five state-owned power groups.
-
NEWSShanglishi Group is the main member appointed by the Pump Association to participate in the development of national standards for slurry pumps and petrochemical centrifugal pumps.
-
CONTACTThe company's good product quality and service have always created value for customers, and are favored by more and more customers.
Six Common Centrifugal Pump Faults, Causes & Troubleshooting Guide
Published:
Oct 30,2026
Analyzing the six major pump malfunctions, tracing their root causes, and ensuring stable operation of the pump unit all hinge on selecting the right equipment based on actual operating conditions.
Pumps are the most unassuming power sources in industrial systems: they operate quietly and often go unnoticed, yet if they stop, the entire process can come to a halt. Below is an overview of six common pump malfunctions and their underlying causes.
Category 1: Insufficient flow rate, reduced head.
When a pump is running but fails to deliver water, or when the system at the far end lacks pressure, the underlying causes can often be summarized in four words: air, blockage, leakage, and corrosion.
Air: This is caused by insufficient priming of the pump or air leaks in the suction line, resulting in residual air inside the pump and causing it to run dry without delivering water.
Clogging: The filter screen, foot valve, or impeller passage becomes blocked by debris, reducing the flow area and preventing adequate flow rate.
Leakage: Excessive wear of the mouth ring clearance leads to increased internal recirculation, causing a simultaneous decline in both flow rate and head.
Cavitation: Insufficient net positive suction head (NPSH) leads to localized vaporization within the pump, forming bubbles that occupy flow passages and cause a simultaneous reduction in both flow rate and head.
Category II: Cavitation Phenomenon
Cavitation is a destructive phenomenon unique to centrifugal pumps and often exhibits a causal relationship with the preceding “corrosion.”
Typical symptoms: the pump body emits a crackling, popping sound; the discharge pressure gauge fluctuates violently; and both flow rate and head decline simultaneously. Upon disassembling the pump casing, the impeller surface often exhibits sponge‑like pitting corrosion.
The energy supplied by the suction system is insufficient to maintain the pressure at the pump inlet above the saturation vapor pressure corresponding to the prevailing temperature. When the available net positive suction head (NPSHa) is inadequate, the liquid boils in low-pressure regions, forming vapor bubbles. As these bubbles enter high-pressure zones, they collapse instantaneously, generating high-frequency water hammer pressures that “erode” the impeller.
Category 3: Vibration and Noise
Vibration is an early warning signal emitted by equipment and a common indicator of various types of faults.
Rotor imbalance, poor alignment between the pump and motor, stress transmitted through the piping to the pump housing, loosened anchor bolts, or prolonged surge in the low-flow region can all cause vibration and abnormal noise.
Category Four: Bearing Overheating
This is the most common cause of unplanned downtime; as temperature rises, component life drops sharply.
Insufficient lubrication or degraded grease, interruption of the cooling water supply, prolonged operation under off‑design conditions resulting in excessive axial loads, or misalignment leading to additional loads on the bearing.
Category 5: Sealing Leaks
Leakage or spray at sealing points not only contaminates the environment but also poses a serious safety hazard due to the release of the process medium.
Dry running of the pump can cause overheating and thermal damage to the sealing faces; particulate‑laden process fluids can erode the sealing surfaces; improper installation compression or a lack of an adequate flushing scheme may also lead to such issues.
Category Six: Power Overload
If the motor current exceeds the limit or the thermal relay trips frequently, never replace the motor with a higher‑rated one without first identifying and addressing the root cause.
Typically, the pump is oversized (with excessive margin), causing it to operate in a high‑flow region beyond its rated capacity and resulting in shaft power overload; alternatively, the density of the conveyed fluid may increase or its viscosity may rise; another possibility is severe mechanical friction within the pump.
Summary
A review of various pump‑unit failures reveals that many potential issues originate during the selection phase. Only by accurately calculating cavitation parameters, matching the medium’s operating conditions, and verifying pipeline constraints can failure risks be mitigated at the source. Making scientifically informed selection based on actual operating conditions is essential to ensuring long‑term, stable pump‑unit performance and achieving cost reduction and efficiency gains.
Shanglish Pump continues to deepen its research into pump‑specific operating conditions and reliable performance, providing tailored pump products and comprehensive solutions for a wide range of industrial fluid‑handling applications.

#Industrial Pump Selection# Industrial Pumps #Six Common Pump Faults# Slurry Pump Operation and Maintenance
Keyword:
Slurry pump,Slurry pump manufacturer,Shijiazhuang slurry pump manufacturer,Scientific selection
SHANGLISHI PUMP GROUP
Department Director: Ms. Wang
Tel: +86-311-82725629
Email: admin@sls-pump.com
WhatsApp: +86 15830676372
Mobile Website
Mobile Website
Copyright © 2022 SHANGLISHI PUMP GROUP
Service